Hey there, if you’re deep into machining, odds are you’ve stumbled across the term “five-axis machining center” before—maybe you’ve heard it’s a game-changer for complex parts, but when it comes to spindle speed, there’s way more to it than a single number. As someone who’s been on the five-axis machining center supplier grind for over 10 years, I get all the questions that pop up when a shop’s first browsing new machines: “What’s the actual spindle speed range I need? Will it work for my job?” Let’s break this down straight, no fancy jargon overload, just the real stuff you care about. Five Axis Machining Center
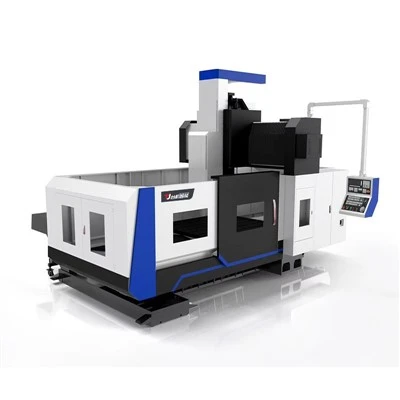
First off, let’s kill a common myth right out the gate: there’s no one-size-fits-all spindle speed range for five-axis machines. Sure, you’ll see generic numbers floating around online, but those are usually for entry-level models built for hobbyists or tiny prototype runs, not the full-size production or high-precision parts most shops are tackling. Spindle speed is measured in RPM (revolutions per minute, for anyone new to the game), and the range on a five-axis machining center is way more dependent on what you’re actually machining than the machine itself.
Let’s start with the basic ranges you’ll typically see across different five-axis machine tiers, because that’s where most people start shopping. Entry-level five-axis models, the ones targeted at small shops or prototypers, usually have a spindle speed range of 100 RPM all the way up to 12,000 RPM. These aren’t built for heavy cuts, though—they’re for soft materials like aluminum, plastic, or even wood for small mold parts. Mid-tier five-axis machines, which are what most job shops and small to medium production runs use, bump that range up to 80 RPM (some even go lower for heavy stock removal) up to 18,000 RPM. Then there are the high-end, production-grade five-axis machining centers, built for aerospace, medical implants, or high-volume automotive parts—their spindle speed ranges go from as low as 50 RPM to a wild 30,000 RPM, and some even hit 40,000 RPM for ultra-fine work on hard metals like titanium.
Wait, but why the big gap between entry and high-end? Let’s get into the why, because that’s what makes this make sense. The spindle’s core is the motor and the bearings, right? Entry-level machines use smaller, less powerful motors with standard ball bearings—they can’t handle sustained high RPM, because that would overheat the spindle or wear out the bearings fast. Mid-tier models use better bearings, often angular contact or even ceramic hybrid bearings, and more robust motors that balance power at low speeds (for hogging out material) with enough oomph at high speeds for finishing cuts. High-end five-axis spindles, though, are usually high-frequency (HF) or liquid-cooled, with precision-machined bearings that can spin fast without vibration—critical for things like milling a hip implant that has to be perfect down to microns.
Now, here’s the part that actually matters for your shop: what spindle speed range do you need, not what the brochure says. Let’s break it down by material, because that’s the biggest factor. If you’re machining soft materials—aluminum, brass, wood, acrylic, even mild plastic—high spindle speed is your BFF. For example, finishing an aluminum aerospace bracket? You’ll want 12,000 to 18,000 RPM to get a smooth surface, avoid tool marks, and cut fast without burning the metal. Soft plastics can actually melt if you go too slow, so 10,000 to 15,000 RPM is standard there.
But if you’re working with hard materials—titanium, Inconel, hardened steel, tool steel—you can’t run high RPM. That’s where the low end of the range matters way more. Machining titanium, for instance, you’ll be running 500 to 1,500 RPM, because high speed would generate way too much heat that wears out your cutting tools instantly. So a five-axis machine for aerospace part manufacturing needs a wide range that can handle both the slow heavy cuts on titanium and the fast finishes on aluminum.
Tool type is another huge factor. If you’re using a small, fine end mill (like a 1mm or 2mm end mill) for intricate detail work—say, a medical component with tiny holes or a gear with small teeth—you need high RPM, like 20,000 to 30,000 RPM, to make the tool cut cleanly without chipping the material. Conversely, if you’re using a large face mill to hog out 2 inches of aluminum from a block, you need low RPM (around 800 to 1,200 RPM) and high torque, even if that’s near the bottom of the spindle range.
Wait, let’s also talk about the mistakes people make when looking at spindle speed. A lot of shop owners think “higher RPM = better,” but that’s only true for specific jobs. If you try to run a heavy cut on titanium at 20,000 RPM, you’ll snap tools, wreck the part, and maybe even damage the spindle. The sweet spot is matching RPM to the material, tool, and cut type, which is exactly why a wide spindle speed range is so valuable for a five-axis machining center—because five-axis machines are used for such a huge variety of parts.
Also, don’t forget about the fifth axis! A lot of people forget that when you’re tilting or rotating the workpiece (that’s the five-axis part), you can get some slight resistance or stress on the spindle at certain angles, especially when cutting off-center. A machine with a flexible spindle range lets you adjust RPM on the fly as you move the axis, so you don’t have to slow down the whole program or risk error when the part is at an angle. I’ve seen shops buy a super expensive five-axis machine with a narrow high RPM range, then get stuck because they can’t slow down enough for heavy titanium cuts—total waste of money.
Let’s talk about what we offer, since I’m coming at this as a supplier, not a random blogger. We build mid to high-tier five-axis machining centers for job shops and medium production runs, so our standard models have a spindle speed range of 60 RPM to 24,000 RPM. Why that number? We did 10 years of field testing with shops that machine everything from aluminum automotive parts to titanium small medical implants. That range gives them enough low-end torque for heavy stock removal on hard metals, and enough high-end speed for fine finishing work on soft materials. We also have a high-performance model for aerospace manufacturers that bumps it up to 50 RPM to 32,000 RPM, with liquid-cooled spindles that can sustain those high RPMs for 8+ hour production runs without overheating.
One question we get all the time: “Can I upgrade the spindle speed later?” Short answer, sometimes, but it’s not worth it. The spindle is one of the core parts of the machine—you can’t just swap out the motor or bearings on an entry-level machine to get a higher range, it’s built into the frame. So when you’re shopping, don’t cut corners here. Figure out the maximum material hardness you’ll work with, and the smallest tool you’ll use, then pick a machine whose spindle range covers both ends of that.
Wait, let’s throw in a quick real-world example to make this concrete. Last year, we worked with a job shop in Detroit that makes both aluminum engine components and small titanium brake caliper parts. They came to us because their old three-axis machine could only hit 10,000 RPM max, which was too slow for finishing the aluminum, and couldn’t drop below 500 RPM, which was too fast for the titanium. They bought one of our mid-tier five-axis machines with the 60 to 24,000 RPM range, and they told us within three months they’d cut tool costs by 28% because they weren’t snapping tools from wrong RPM settings, and their production output went up 40% because they could run both jobs on the same machine, no more switching between machines. That’s the real payoff of a well-matched spindle speed range.
Another common point: spindle speed isn’t the only factor, but it’s a critical one paired with power. A machine can have a 50 to 30,000 RPM range, but if its motor doesn’t have enough torque at low RPM, it’ll struggle to cut hard materials. So when you’re comparing numbers, don’t just look at the top RPM—ask about the torque curve. That’s how much power the spindle has at different RPMs, which is way more useful than just the max RPM. For example, a good five-axis spindle will have 90% of its peak torque available at 1,000 RPM, so you can do heavy cuts without losing power.
Let’s also address entry-level hobbyist machines, just to be thorough. If you’re a maker or a small shop doing one-off prototypes, you might see five-axis machines with 100 to 12,000 RPM ranges. Those work for soft materials, small tools, and low volume, but if you’re looking to make money machining, that range will limit you hard. You won’t be able to take on aerospace or medical jobs, you’ll wear out the spindle fast if you push it, and you’ll hit a ceiling on production volume.
So putting it all together, the spindle speed range of a five-axis machining center isn’t a fixed number—it’s a spectrum tailored to the machine’s tier, design, and intended use. Entry-level: 100–12,000 RPM, mid-tier: 60–24,000 RPM, high-end production: 50–32,000 RPM. But the only range that matters for your shop is the one that covers the materials, tools, and jobs you actually do.
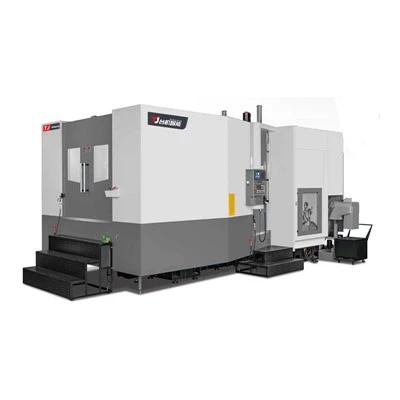
If you’re in the market for a new five-axis machining center and want to stop guessing if your spindle speed range will work for your line of work, reach out. We’ve helped hundreds of shops—from prototypers to high-volume production facilities—match the right spindle specs to their needs, no sales pressure, just honest advice. We can send you case studies, breakdowns of our different machine lines, and even help you calculate exactly what RPM range you need based on your typical jobs. Don’t waste money on a machine that can’t handle your work—let’s chat and get you set up with a five-axis machining center that fits.
Five Axis Machining Center References
- Modern Machine Shop. (2022). Five-Axis Machining: Capabilities, Applications, and Performance Specifications. Gardner Business Media
- SME (Society of Manufacturing Engineers). (2021). Spindle Technology for High-Precision Machining. SME
- machiningcloud.com. (2023). Spindle Speed Selection Guide for CNC Machining. Machining Cloud Inc.
Guangdong Taiji Intelligent Equipment Co., Ltd.
With abundant experience, we are one of the most professional five axis machining center manufacturers and suppliers in China. Please feel free to buy cheap five axis machining center for sale here from our factory. For price consultation, contact us.
Address: Room 107, Building 15, No. 911 Jian’an Road, Chang’an Town, Dongguan City, Guangdong Province
E-mail: sale@gdtaijicnc.com
WebSite: https://www.gdtaijicnc.com/
