If you’ve ever stood in a bustling commercial building, a cozy residential high-rise, or a sprawling industrial facility, you’ve likely taken for granted the steel shaft elevator that glides you from floor to floor. As a supplier of these critical vertical transport systems, I field questions all the time: why do steel shaft elevators cost what they do? What’s hidden in the price tag beyond the obvious “metal box that goes up and down”? Let’s break down the real, practical cost components that go into every steel shaft elevator we deliver—no corporate jargon, just the facts we walk through with every customer who’s ever stared at a quote and wondered where every dollar went. Steel Shaft Elevator

First, let’s get clear on what a steel shaft elevator actually is, for anyone new to the space. Unlike the old-style traction elevators that use ropes and a separate overhead machine room, modern steel shaft elevators integrate the structural shaft (the vertical track system that contains the elevator) directly into the steel framework of a building, with the lift components mounted right within that shaft. That design cuts down on construction time and frees up valuable floor space—two huge selling points for projects of all sizes. But that design also means every part of the system is tailored to fit the specific project, not off-the-shelf, which is why cost breakdowns aren’t one-size-fits-all.
Starting with the biggest, most foundational cost: structural shaft fabrication and materials. This isn’t just a pipe dream—this is the backbone of the entire elevator. Unlike a generic steel beam, elevator shaft steel has to meet rigorous load requirements. The shaft has to support the full weight of the elevator cab, plus 80% of its maximum rated capacity (wait, no, actually, code requires it to support up to 125% of the rated load for safety margins) and account for dynamic forces every time the elevator starts or stops. That means we use high-strength carbon steel, not the thin metal you’d use for a backyard shed. The steel is cut, bent, and welded at our in-house fabrication shop to precise tolerances—within a millimeter of accuracy, because even a slight misalignment can cause the elevator to jostle or wear out parts prematurely. For a mid-rise building (say, 10 floors, 3,000 pounds capacity), that steel can run anywhere from $15,000 to $25,000, depending on how complex the shaft shape is. If the building has unique floor plans—like sloped ceilings or irregular corner layouts—we have to custom-cut every steel panel, which adds labor time and extra material costs. We’re talking about 12 to 18 hours of skilled fabricator time alone for that mid-rise shaft, and skilled welders aren’t cheap. They don’t just tack pieces together—they have to test each weld for defects, grind them smooth, and apply a corrosion-resistant coating (hot-dip galvanizing, usually, which adds another 10-15% to the steel cost) to prevent rust in high-humidity environments, like coastal areas or underground parking garages.
Next, the core lift system: the traction or hydraulic components? Wait, no—steel shaft elevators can be either, but most modern ones use roped traction systems with a compact machine room, or machine-room-less (MRL) systems, which are more popular for mid and high-rises. Wait, let’s clarify that. For traction-based steel shaft elevators, the hoisting machinery is the next big cost. The hoist motor, gearbox (or gearless drive, for smoother operation), and the pulleys that the steel cables wrap around have to be sized for the elevator’s load and speed. A 3,000-pound capacity elevator moving at 150 feet per minute needs a 5-horsepower gearless traction drive, which costs around $8,000 to $12,000. If the client wants a higher speed—say, 250 feet per minute for a 15-floor building—that jumps to $15,000 or more. Then there are the steel ropes themselves. We don’t use regular twine, obviously. Elevator cables are made of multiple strands of high-tensile steel, twisted together to handle the 20,000 to 50,000 pounds of tension they’re under every time the elevator travels. For a mid-rise elevator, we use 8 to 10 of these cables, each costing roughly $150 per hundred feet, and they have to be inspected and tested to meet ASME A17.1 codes, the strict safety standard for elevators in North America. That’s another $2,000 to $4,000 for the cables alone.
Wait, for applications where a hydraulic system makes more sense—like low-rise residential buildings (2 to 5 floors)—the core cost shifts to the hydraulic pump, cylinder, and fluid. A 2,000-pound hydraulic steel shaft elevator for a small apartment building might have a core lift system cost of $6,000 to $9,000. But regardless of traction or hydraulic, there’s the control system, which is the brain of the elevator. I can’t stress how important this is. The control panel regulates when the elevator moves, how fast it accelerates, how it responds to call buttons, and most critically, it has a dozen safety features built in: overload sensors, door obstruction detectors, emergency brake systems, and communication links to 911 or building management. We use PLC (programmable logic controller) systems, not the cheap knockoffs you might find online, because knockoffs don’t meet safety codes and have a 5-year failure rate instead of the 15+ years we expect from our systems. A mid-rise elevator control panel runs $3,000 to $5,000, and that includes the software programming, which takes our engineers 20 to 30 hours to customize for each project. We also have to integrate it with the building’s fire safety system, so the elevator automatically returns to the ground floor if a fire alarm goes off—another layer of customization and code compliance that adds to the cost.
Then there’s the cab and interior finishes, which might seem like a cosmetic part, but they’re a big selling point for commercial and residential projects. The cab has to be durable, first and foremost. A steel cab frame is standard, but the interior panels can be stainless steel, drywall, wood veneer, or even glass, depending on the client’s design. For a commercial office building, clients usually opt for brushed stainless steel, which is easy to clean and resists scratches. A standard stainless steel cab for a mid-rise elevator costs $4,000 to $6,000, but if they want a custom wood ceiling, LED lighting, or a touch-screen destination control panel, that can add another $2,000 to $10,000 or more. We also have to include the doors, which are a separate cost. Elevator doors aren’t just metal slabs—they’re powered by motors, have safety edges that reverse if something gets caught, and are sized to fit the shaft. A pair of automatic sliding doors for a mid-rise elevator is $3,000 to $5,000, and if they’re fire-rated (required for many commercial buildings), that adds another 20% to the cost. The doors have to meet fire-resistance codes, so they’re made with fire-rated steel and close automatically during a fire—another safety requirement that’s non-negotiable.
Wait, let’s not forget installation. No one can just drop a steel shaft elevator into a building and call it done. Our installation teams are certified, they work around construction schedules, and they have to coordinate with the general contractor, electricians, and plumbers. Installing a steel shaft elevator is not like assembling a bookshelf. For a mid-rise building, installation takes 4 to 6 weeks, with a team of 3 to 5 certified technicians, each making well above the average construction wage (they’re specialized, after all). Installation costs can run anywhere from $10,000 to $20,000 for a mid-rise elevator, depending on how accessible the shaft is. If the building is still under construction and we can hoist parts in through the roof, it’s cheaper, but if we have to bring parts in through narrow hallways and up stairs, that adds extra labor time and cost. We also have to do the final inspections by local code officials—we don’t just let the client use it until the city signs off. The inspection fees are part of the process, too, usually a few hundred to a thousand dollars, depending on the location.
Safety is a cost component that many clients overlook at first, but it’s the most important one. Every part of our steel shaft elevators meets not just local codes, but national safety standards. We have emergency stop buttons that work, interlock systems that keep the elevator from moving if the doors are open, backup power systems (batteries) that let the elevator get stuck passengers to safety during a power outage, and regular maintenance plans that we offer for 10+ years after installation. The backup battery system alone for a mid-rise elevator is $1,500 to $2,500, and that’s non-negotiable. In some states, like California, there are additional seismic safety requirements for elevators, so we have to add seismic bracing to the shaft, which adds another 10-15% to the structural shaft cost. I’ve seen clients try to skip safety features to save money, but it always comes back to bite them. Last year, we had a client in Oregon who opted for a cheaper control system that didn’t meet seismic codes, and he had to replace it 2 years later at a cost three times the original difference.
Customization and logistics also play a big role. Not every project is the same. A steel shaft elevator for a hospital needs to be wheelchair-accessible, have a wider cab to stretch stretchers, and be quieter so it doesn’t disturb patients. That means custom cab dimensions, reinforced steel to handle the extra weight, and a sound-dampening system under the cab, adding $5,000 to $8,000 to the cost. For a historic building, we might have to design a shaft that fits around existing architectural features, which requires more engineering time and custom steel fabrication, adding 15-20% to the total. Logistics, too: if the project is in a remote area, like a mountain resort or a small town, we have to ship the steel parts, which are heavy, so freight costs can add $2,000 to $5,000, depending on the distance.
Wait, let’s add up the numbers to put it in perspective. For a mid-rise steel shaft elevator (10 floors, 3,000 lb capacity, commercial grade), the total cost usually breaks down like this: structural shaft fabrication $20,000, core lift system $10,000, control system $4,000, cab and doors $5,000, installation $15,000, safety and code compliance $5,000, customization and contingency $6,000. That adds up to around $65,000 for a basic system, but it can go up to $100,000 or more for high-end, custom projects like a luxury residential building or a hospital elevator. For a small, low-rise residential elevator (2 floors, 2,000 lb capacity), it’s much lower—around $25,000 to $35,000.
I’ve been in this business for 12 years, and one thing I’ve learned is that every cost component is there for a reason. It’s not just about buying steel parts and putting them together. It’s about making a system that’s safe, reliable, and will last 20 to 30 years, even with daily use. Too often, clients get tempted by cheap quotes from companies that cut corners—using low-grade steel, uncertified parts, or untrained installers. Those systems might work for a few years, but they break down constantly, require expensive repairs, and can pose safety risks. Last year, we had a client who went with a competitor’s quote that was $15,000 lower than ours. Two years later, their elevator had a cable break (thankfully, no one was hurt) because the competitor used cheap steel cables that didn’t meet code. They ended up paying $20,000 in repairs and fines, plus the cost of a new elevator because the entire system was defective. That’s the real cost of cutting corners.
So if you’re planning a project that needs a steel shaft elevator, don’t just look at the upfront price. Ask for a detailed breakdown of each component: what grade steel is used, what safety certifications the parts have, who will install it, and what the maintenance plan is. We provide our clients with a full, line-item quote so they know exactly where every dollar goes—no hidden fees, no surprise costs. We work with architects, general contractors, and building owners to design a steel shaft elevator that fits their needs and their budget, without sacrificing safety or quality.
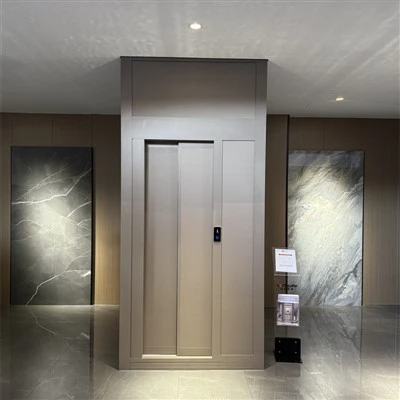
If you’re ready to discuss your next project, or have questions about the cost components of a steel shaft elevator, we’d love to hear from you. Whether it’s a small residential building, a commercial office, or an industrial facility, we have the expertise to deliver a system that’s reliable, code-compliant, and built to last. Reach out to us today to start the conversation, and we’ll provide you with a custom quote tailored to your project’s needs.
Concrete Shaft Elevator References
ASME A17.1 – Safety Code for Elevators and Escalators
Steel Construction Manual, American Institute of Steel Construction (AISC), 15th Edition
Elevator Industry Association (EIA) Technical Guidelines for Steel Shaft Elevator Systems
International Building Code (IBC) 2021, Chapter 30: Elevators, Escalators, and Conveying Systems
Zhejiang Homeway Elevator Co., Ltd.
Zhejiang Homeway Elevator Co., Ltd. is one of the most professional steel shaft elevator manufacturers and suppliers in China. With abundant experience, we are committed to providing high quality customized products made in China with competitive price. If you’re going to buy CE approved steel shaft elevator, welcome to get quotation from our factory.
Address: No.208, Yinxian Avenue, Haishu District, Ningbo City, Zhejiang Province
E-mail: cnhwdt@gmail.com
WebSite: https://www.homewayelevator.com/
