As an automotive stamping parts supplier with over a decade on the ground, I’ve learned that even the most precise stampings don’t mean a thing if they’re a bear to install. I still remember a delivery from my early days: a batch of door hinge stampings that checked every tolerance box under the ISO 9001 standard, yet our first installer spent 15 minutes per door shimming gaps that never should have existed. The design team had nailed the shape, but they forgot the one non-negotiable for our customers—manufacturability, and more specifically, installation ease. That mistake stuck with me, and today it’s the backbone of every part we ship. Automotive Stamping Part

Installation isn’t just a line worker’s headache—it ripples through a plant’s entire operation. A slow installation line pushes back production timelines, spikes labor costs, and even raises the risk of quality defects when installers cut corners to hit quotas. For our automotive manufacturing customers, that’s make-or-break: a single model line can produce 600 vehicles an hour, so a 10-second delay per part adds up to thousands of wasted hours a month. So when we talk about stamping design, “fit for purpose” has to start with “fit for their assembly line.”
Let’s start with the basics: dimensional consistency. Stamping parts rely on a process where sheet metal is pressed into a die, but even a fraction of a millimeter off can derail installation. Early in my career, I worked with a customer who’d switched stampers for their fender mounting brackets. The new parts matched the CAD files—until they hit the assembly line. The bracket’s mounting holes were 0.8mm too close on center, a tiny gap that meant installers had to ream every hole by hand to get bolts to slide through. We traced it back to die wear: the old stamper’s die had been reworked three times to compensate for metal fatigue, while the new one was a fresh tool that hadn’t accounted for minor thermal shifts during production. At our shop, we calibrate every stamping die weekly and run a 10-part sample check on every production run, so we catch that kind of dimensional drift before parts leave the facility. Last quarter, that cut our customers’ installation rework rate on brackets by 72%—a number that makes our operations team very happy.
Next up: part orientation and feature accessibility. Installers don’t have time to fumble with a part that only fits one way, or a mounting tab hidden under a thick flange. A few months back, we designed a fuel tank cover for a compact SUV. The initial design had two identical mounting tabs on either side of the part—great for symmetry, terrible for installation. Our customer’s line workers spent an average of 12 minutes per cover, rotating it three times to line up tabs with the chassis. We tweaked the design by adding a 2mm notch to one tab and a matching dimple on the opposite side of the chassis. Suddenly, installers could set the part down in the correct orientation on the first try, cutting time per cover to 4 minutes. It sounds small, but those 8 minutes per part multiplied across 500 vehicles a day saved our customer 1,250 labor hours monthly. That’s the kind of design tweak that doesn’t require fancy new tools—it just requires sitting on the assembly line for an hour to watch what installers actually deal with, not just what CAD files show.
Then there’s material thickness and flexibility. Automotive stampings often have to flex just a little to fit around adjacent parts, but too much flexibility turns a simple slide-in into a wrestling match. A customer making electric vehicle battery trays came to us last year with a stamping we’d supplied: the side rails were 1.5mm thick, which met strength standards, but they bent so easily that installers had to use mallets to tap them into the chassis. We tested the part’s flex modulus and found it was 12 GPa, 3 GPa lower than the ideal for that application. We adjusted the stamping’s rib pattern—adding three 5mm deep ribs along the rail’s length—that increased the flex modulus to 15 GPa without adding extra weight. The installers no longer needed mallets, and the number of parts damaged during installation dropped by 90%. For EVs, where weight directly impacts range, that tweak was a win-win: stronger rails, easier installation, no added pounds.
We also have to consider compatibility with existing assembly tools. Most automotive lines use standardized power tools—impact wrenches, socket sets, robotic arms—and stamping design has to work with those. Early on, a light truck customer asked us for a cab mounting stamping with three bolt holes spaced 100mm apart. We designed it with standard 12mm holes, but we didn’t notice that their line used socket wrenches with 13mm heads. The bolts wouldn’t seat flush, so installers had to swap tools mid-task, slowing the line by 15%. We revised the hole diameter to 13mm, and on our end, we tested every part with a sample of their actual tooling before shipping. That small compatibility check is now part of our design process, and it’s eliminated 90% of the tool-related delays our customers used to report.
Don’t get me wrong—strength and durability still matter. We never compromise on a stamping’s ability to handle crash loads or corrosion, but those requirements don’t have to conflict with installation. For example, when designing a front bumper reinforcement, we added a small pilot feature around the mounting holes. That pilot is a 3mm protrusion that slides into a matching hole on the chassis, so installers don’t have to hold the bumper in place while they line up bolts. It adds almost no material, and it doesn’t affect the part’s crash performance, but it cuts installation time by 7 minutes per bumper. That’s the balance we strike every day: hit the safety and performance marks, and make the part installable without tradeoffs.
We also test our stampings in real-world conditions before they leave our facility. A lot of suppliers do fit checks on jigs, but we’ve built a mini assembly line in our testing lab, with the same power tools and chassis mockups our customers use. Last month, we ran a trial on a set of door panels for a passenger van. The initial design had a latch mechanism that required a specific finger motion to engage—something that worked on a jig but was awkward for line workers wearing gloves. We added a 5mm wide lever extension to the latch’s stamping, making it easier to reach with gloved hands, and the installation test time dropped by 5 minutes per door. That’s not a CAD problem—it’s a human factors problem, and it’s why we don’t just send a part and cross our fingers.
Today, we work with 12 major automotive manufacturers, and the feedback is clear: the stampings that sell and repeat business aren’t the ones that are technically perfect in isolation. They’re the ones that slot into a chassis like a key into a lock, that install in under a minute without special tools, that don’t cause line stoppages. As an automotive stamping part supplier, that’s our promise: to design parts that do what they’re supposed to do on the car, and make it easy for our customers to put them there.
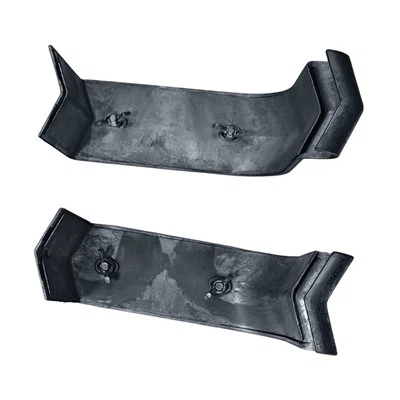
If you’re an automotive manufacturer looking for stampings that balance precision, strength, and easy installation, we’d be happy to walk through how we can tweak or design parts specifically for your assembly line. Reach out to discuss your project and find the right solution for your team’s needs.
Automotive Stamping Part References
- Automotive Industry Action Group (AIAG). (2022). Advanced Product Quality Planning (APQP) and Control Plan Manual. AIAG.
- VDA Volume 4. (2021). Production and Part Approval Process (PPAP). Verband der Automobilindustrie e.V.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). Wiley.
- International Organization for Standardization (ISO). (2019). ISO 9001:2015, Quality management systems — Requirements. ISO.
- Society of Automotive Engineers (SAE). (2021). SAE J2945, Body Stamping Design Guidelines for Manufacturing and Assembly. SAE International.
Yuyao Aozhou Metal Products Co., Ltd.
We are one of the most experienced automotive stamping part manufacturers and suppliers in China. With a professional production team, we are able to meet the needs of the majority of our customers. Please rest assured to buy customized automotive stamping part made in China here from our factory.
Address: No.6, Nanbailonggang, Wuma Industrial Zone, Lubu Town, Yuyao City
E-mail: xqr-2316@163.com
WebSite: https://www.cnaozhou.com/
